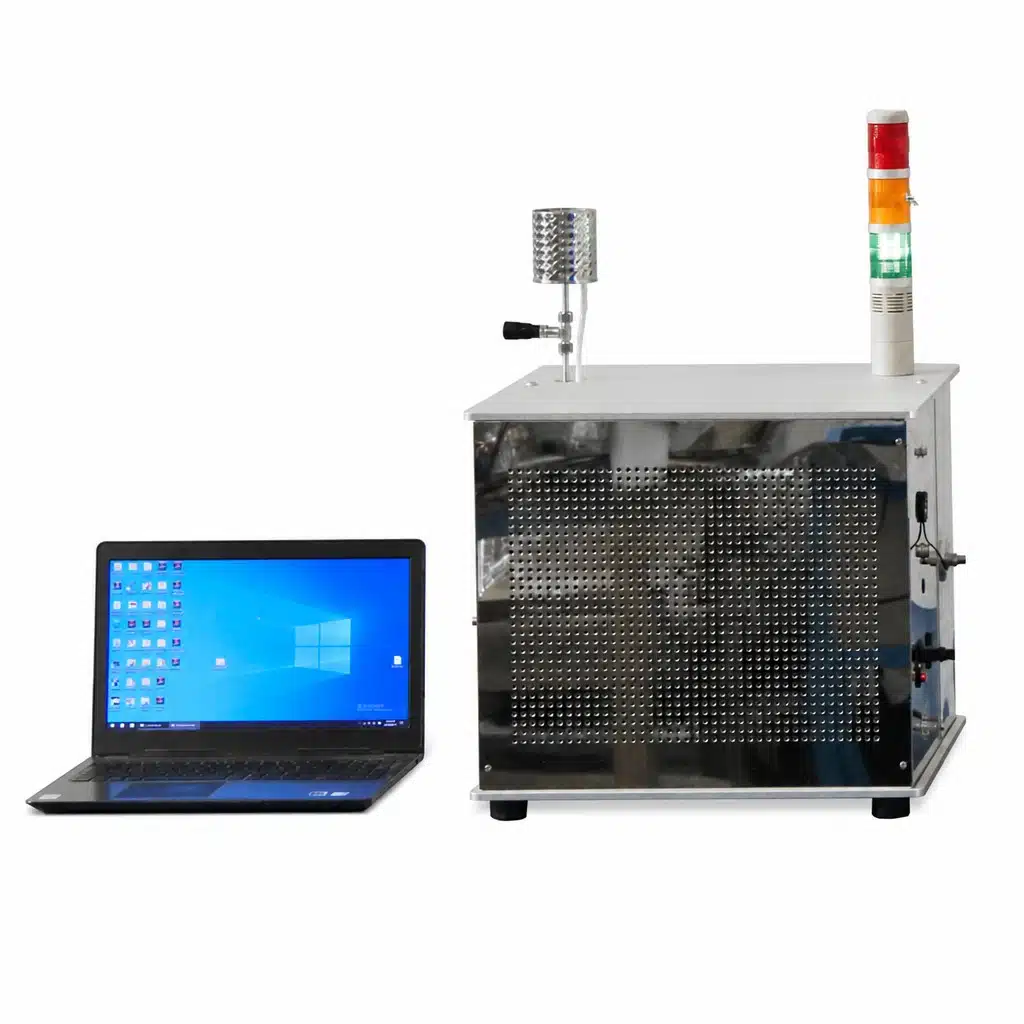
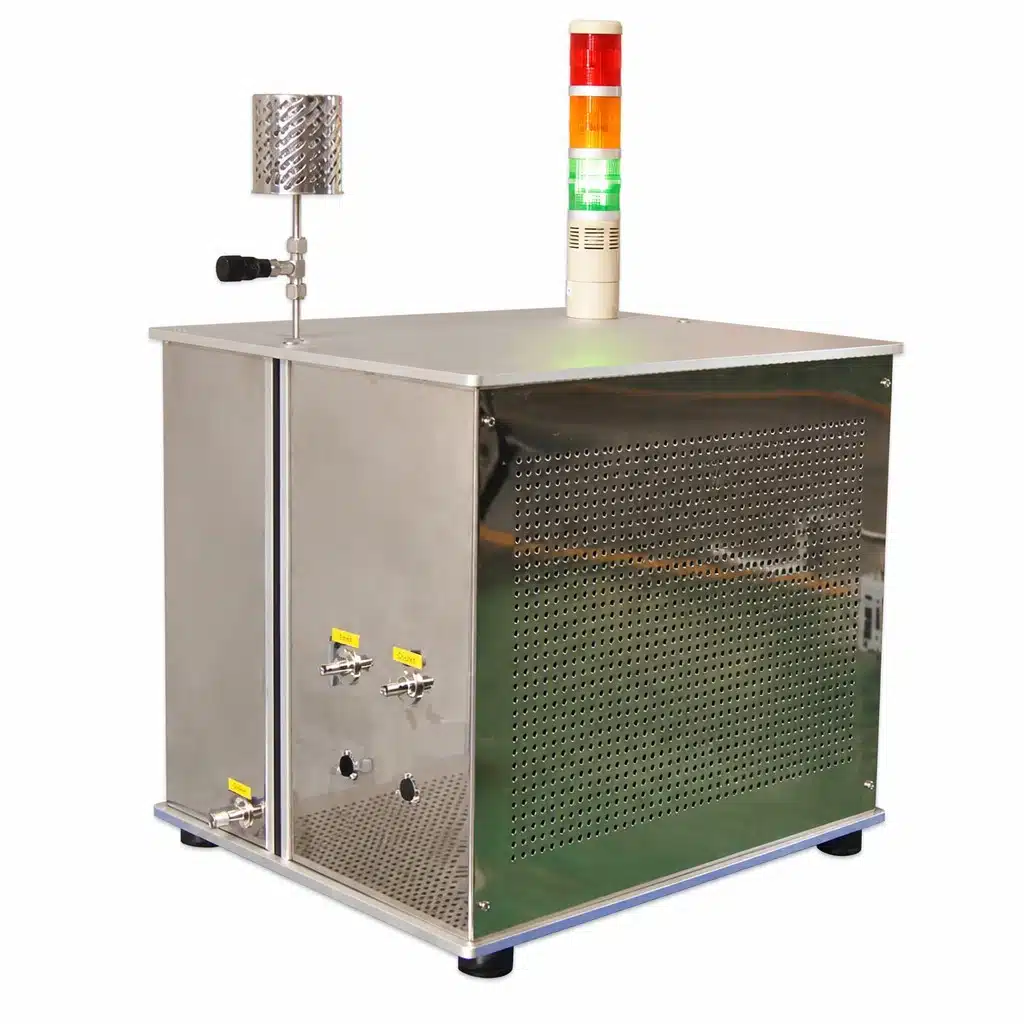
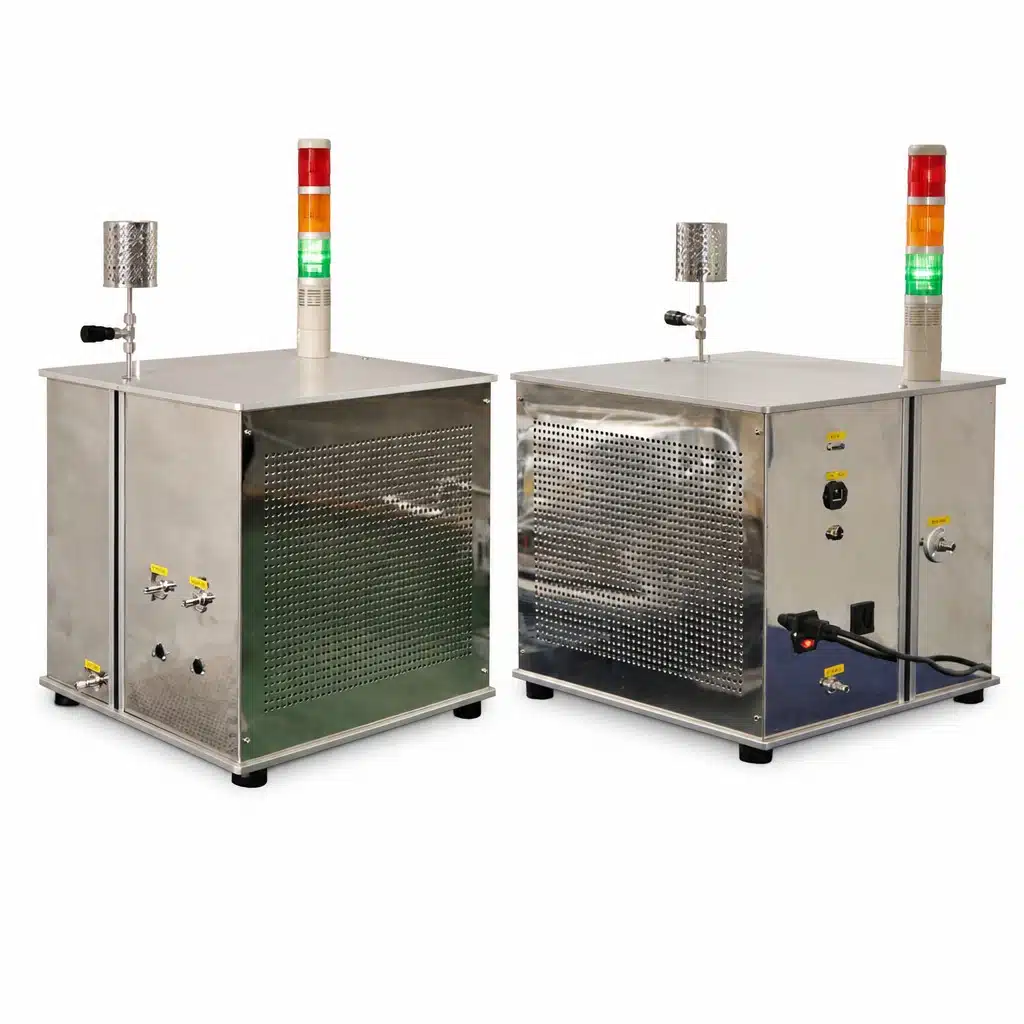
GSL-KR100 Automatic Flammable Gas Control and Disposal Device with Self-Ignition Heating Coil and Remote Monitoring
The GSL-KR100 is engineered to manage and safely eliminate residual flammable gases generated during laboratory processes, particularly in experiments involving reducing atmospheres such as hydrogen flow. It is designed to integrate seamlessly with MTI tube and atmosphere furnaces, providing a controlled environment by combusting leftover flammable gases through a self-ignition heating coil.
This device not only disposes of hazardous gases but also offers precise gas flow regulation and safety interlocks. It communicates with a Honeywell hydrogen gas detector to monitor gas leaks and automatically shuts off gas flow and furnace heating in emergency conditions. Remote operation and data logging are facilitated via an RJ45 Ethernet port, enhancing laboratory safety and control.
Key Features
- Self-ignition heating coil for combustion of residual flammable gases.
- Compatible with MTI tube and atmosphere furnaces for reducing environment experiments.
- Gas flow control with a mass flow controller ranging from 0 to 1000 sccm.
- Integration with Honeywell hydrogen gas detector with preset alarm at 20% LEL.
- Safety interlocks that cut off gas flow and furnace heating upon gas leak detection, coil failure, overpressure, or absence of flammable gas flow.
- Dual solenoid valves to select between inert and flammable gas flow paths.
- Double explosion protection via pressure sensor and mechanical pressure relief valve.
- Remote control, monitoring, and data logging through RJ45 Ethernet connection.
- Constant pressure mode to maintain slightly positive pressure in the furnace tube during heating.
Technical Specifications
| Parameter | Specification |
|---|---|
| Power | 200 W |
| Voltage | 110 V, 208-240 VAC, Single Phase, 50/60 Hz |
| Gas Flow Rate | 0-1000 sccm |
| Gas Inlet | Two 1/4″ compression tube fittings (for inert and flammable gases) |
| Hydrogen Gas Detector | Connected to control box; alarm preset at 20% LEL; triggers shutdown of gas flow and furnace heating |
| Overpressure Protection | Electronic pressure transmitter activates exhaust valve; mechanical pressure relief valve at 0.4 bar relative pressure |
| Control Interface | RJ45 Ethernet port for remote control, monitoring, and data logging |
| Operating Modes | Manual and automatic purging; constant pressure sintering mode (100,000 Pa to 115,000 Pa) |
Typical Applications
Ideal for laboratory experiments requiring safe disposal of flammable gases, especially in reducing atmospheres such as hydrogen flow during sintering or material processing. Suitable for integration with MTI tube and atmosphere furnaces to enhance safety and environmental control.
Configuration & Operating Notes
The GSL-KR100 requires installation of a metallic mesh cover at both ends of the furnace tube when used with tube furnaces to ensure emergency containment. It must be operated in a well-ventilated area or fume hood. The hydrogen gas detector is mandatory for safe operation. Operators should be trained by qualified personnel and adhere strictly to laboratory safety guidelines. Optional accessories and consumables such as heating elements, processing tubes, and O-rings are available separately.
Dimensions & Shipping
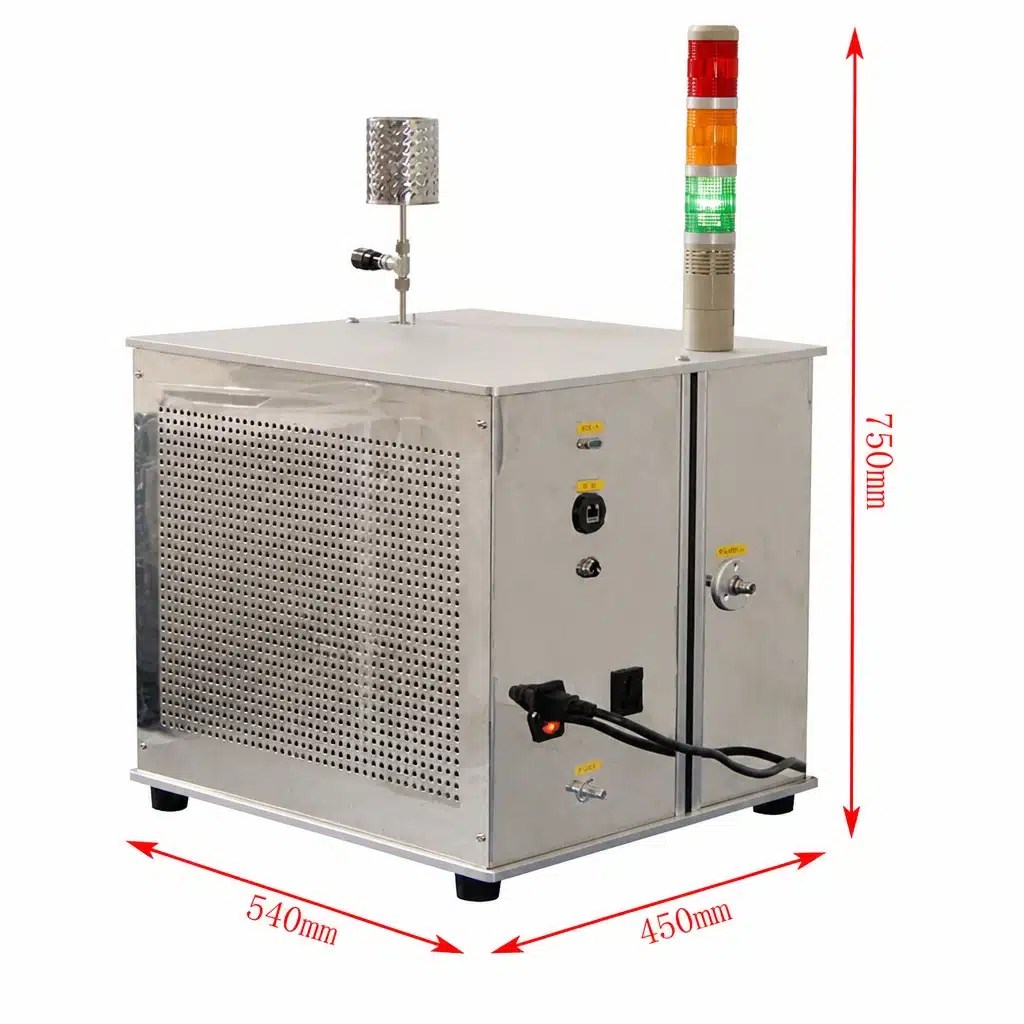
| Product dimensions | 500L × 450W × 750H (mm) |
|---|


