MSK-SFM-50L-TE Automatic 50L Liquid Phase Reactor with Heating and pH Control for Ternary Precipitation
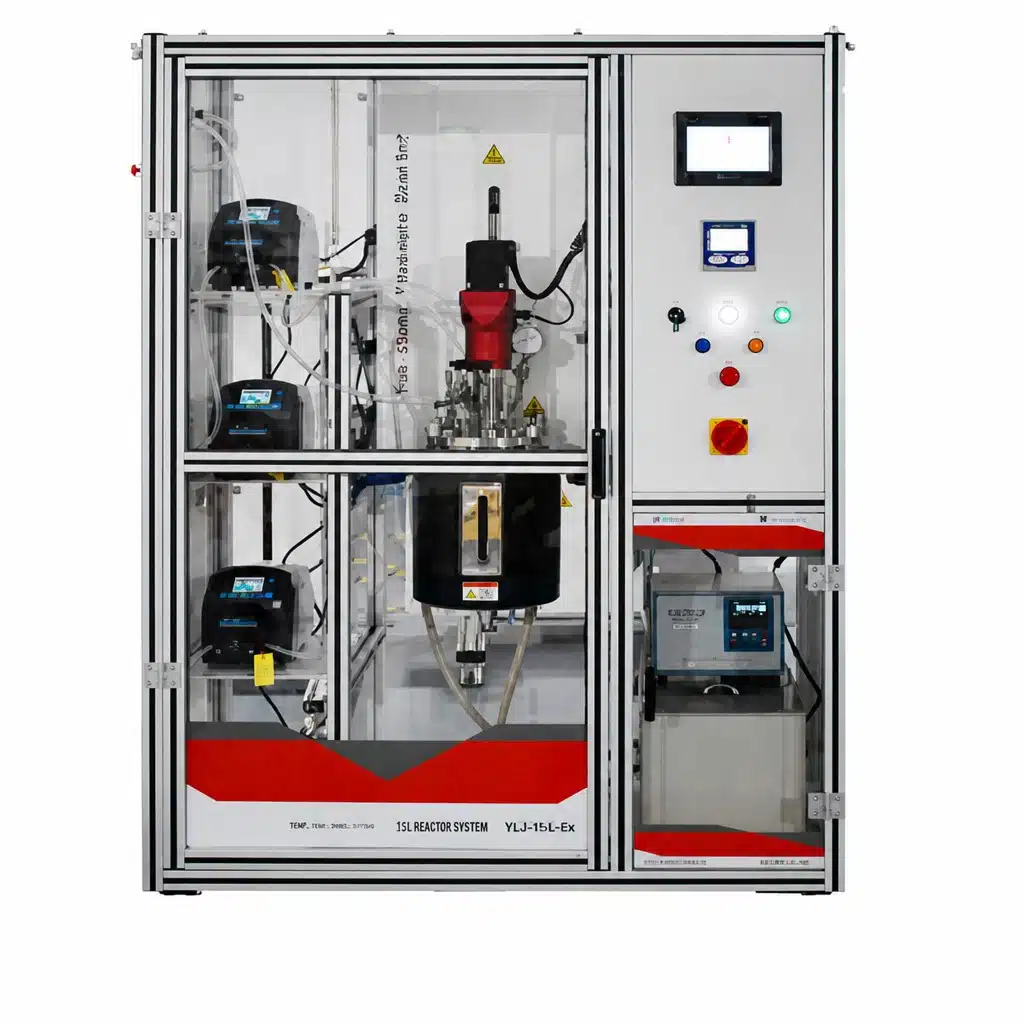
The MSK-SFM-50L-TE reactor is engineered for pilot-scale synthesis of uniform ternary liquid phase systems, particularly suited for co-precipitation processes in battery material and complex compound preparation. Its 50-liter capacity allows for effective wet chemical synthesis of ternary system powders under controlled conditions.
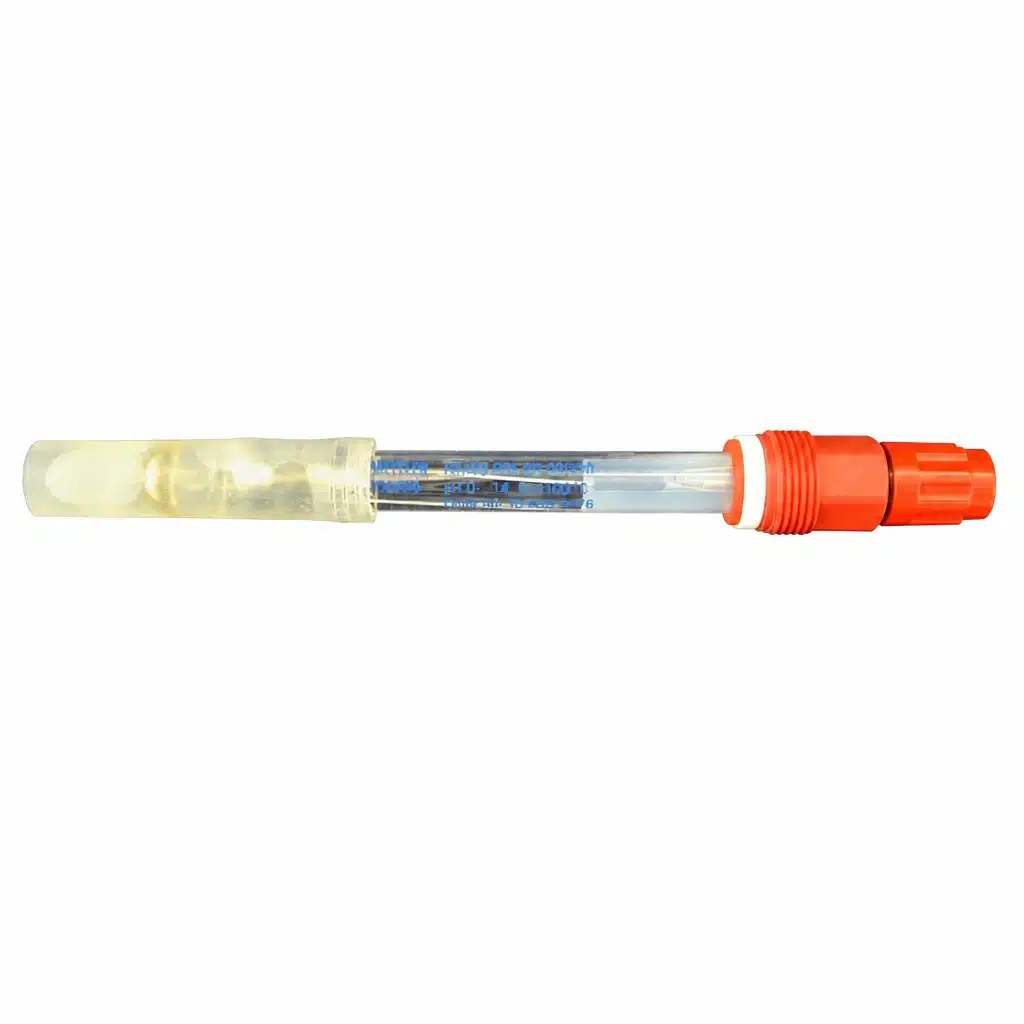
This reactor integrates precise temperature regulation via a recirculating hot water bath, maintaining temperatures from ambient up to 90°C with ±0.5°C accuracy. The system also features automatic pH control through a Mettler pH transmitter and three digitally controlled peristaltic pumps that add or reduce acid or alkaline solutions as programmed, ensuring stable reaction conditions.
Key Features
- 50-liter double-layer stainless steel reactor (SS 316 inner vessel, SS 304 cooling jacket) with mechanical stirring blades made of SS 316L.
- Temperature control via recirculating water bath with PT100 thermocouple sensor, accurate to ±0.5°C, max 90°C.
- Automatic pH regulation using a Mettler pH transmitter and three digital peristaltic pumps delivering solutions at rates up to 2.3 L/h with 2% accuracy.
- 7-inch color touchscreen panel for setting and monitoring pH, stirring speed (0-500 rpm), liquid flow rates, and temperature.
- Multiple ports including three feeding ports, two gas inlets/outlets, sampling port, and drainage for continuous feeding and draining during co-precipitation.
- Adjustable stirring blade positions to optimize mixing efficiency.
- Power supply: 208-240 VAC, single phase, 50/60 Hz; total power consumption 5,750 W.
Technical Specifications
| Parameter | Specification |
|---|---|
| Reactor Volume | 50 Liters |
| Reactor Material | Inner vessel SS 316, Cooling jacket SS 304 |
| Reactor Dimensions | Ø400 × 500 mm |
| Temperature Range | Room Temperature to 90°C |
| Temperature Sensor | PT 100 Thermocouple |
| Temperature Accuracy | ±0.5°C |
| Stirring Speed | 0 – 500 rpm, adjustable blade positions |
| Peristaltic Pump Rate | 0 – 2.3 L/h per pump |
| Pump Accuracy | ±2% Full Scale |
| pH Control | Automatic via Mettler pH transmitter |
| Control Interface | 7″ color touchscreen panel |
| Power Supply | 208 – 240 VAC, single phase, 50/60 Hz |
| Total Power | 5,750 W |
Typical Applications
Ideal for pilot-scale synthesis of uniform ternary liquid phase systems used in battery electrode material development, complex compound preparation, and wet chemical co-precipitation processes.
Configuration and Operating Notes
The system requires three separate SS316 50-liter containers (not included) to supply the different solutions via the peristaltic pumps, as well as one container for draining the reactor output. These containers must be ordered separately. The reactor includes multiple ports for feeding, gas inlet/outlet, sampling, and drainage to facilitate continuous operation. A power cable is included, but the plug is not supplied. Compliance includes CE certification, with NRTL or CSA certification available upon request at additional cost.


